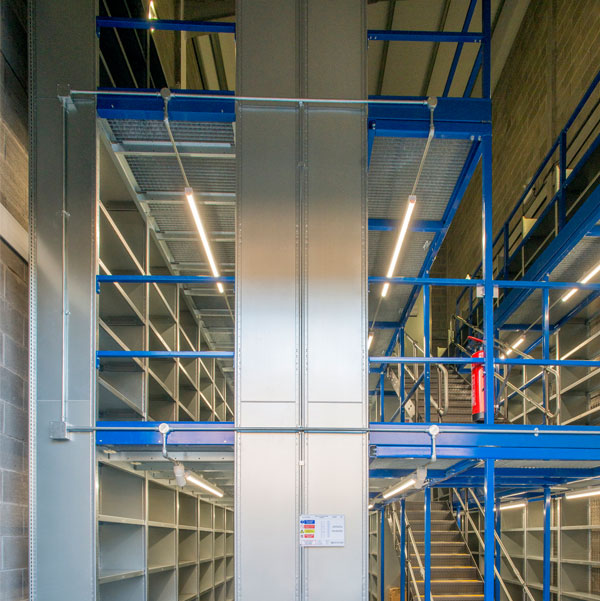
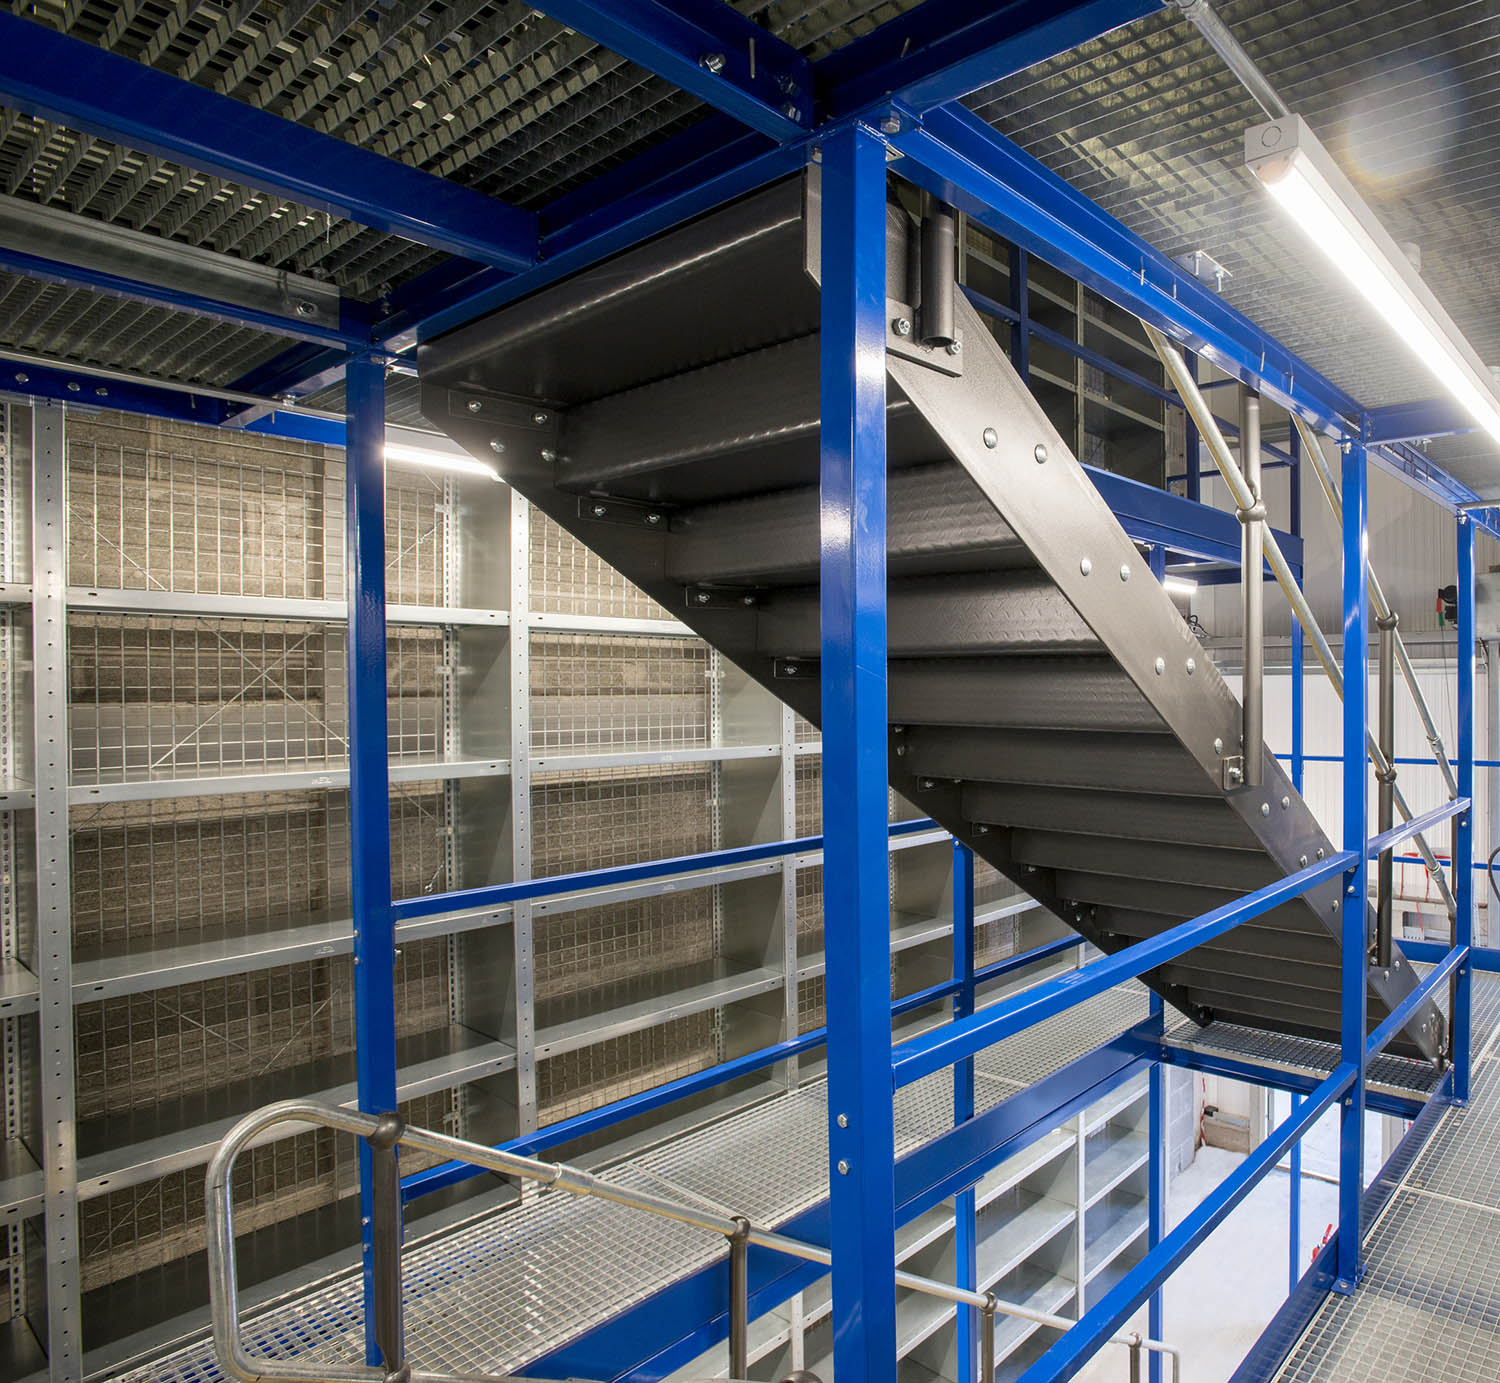
Thistle Systems has enabled a major Scottish distiller to transform its label and sample stores by designing, supplying and installing a three storey Picking Tower to maximise capacity in the available floor space.
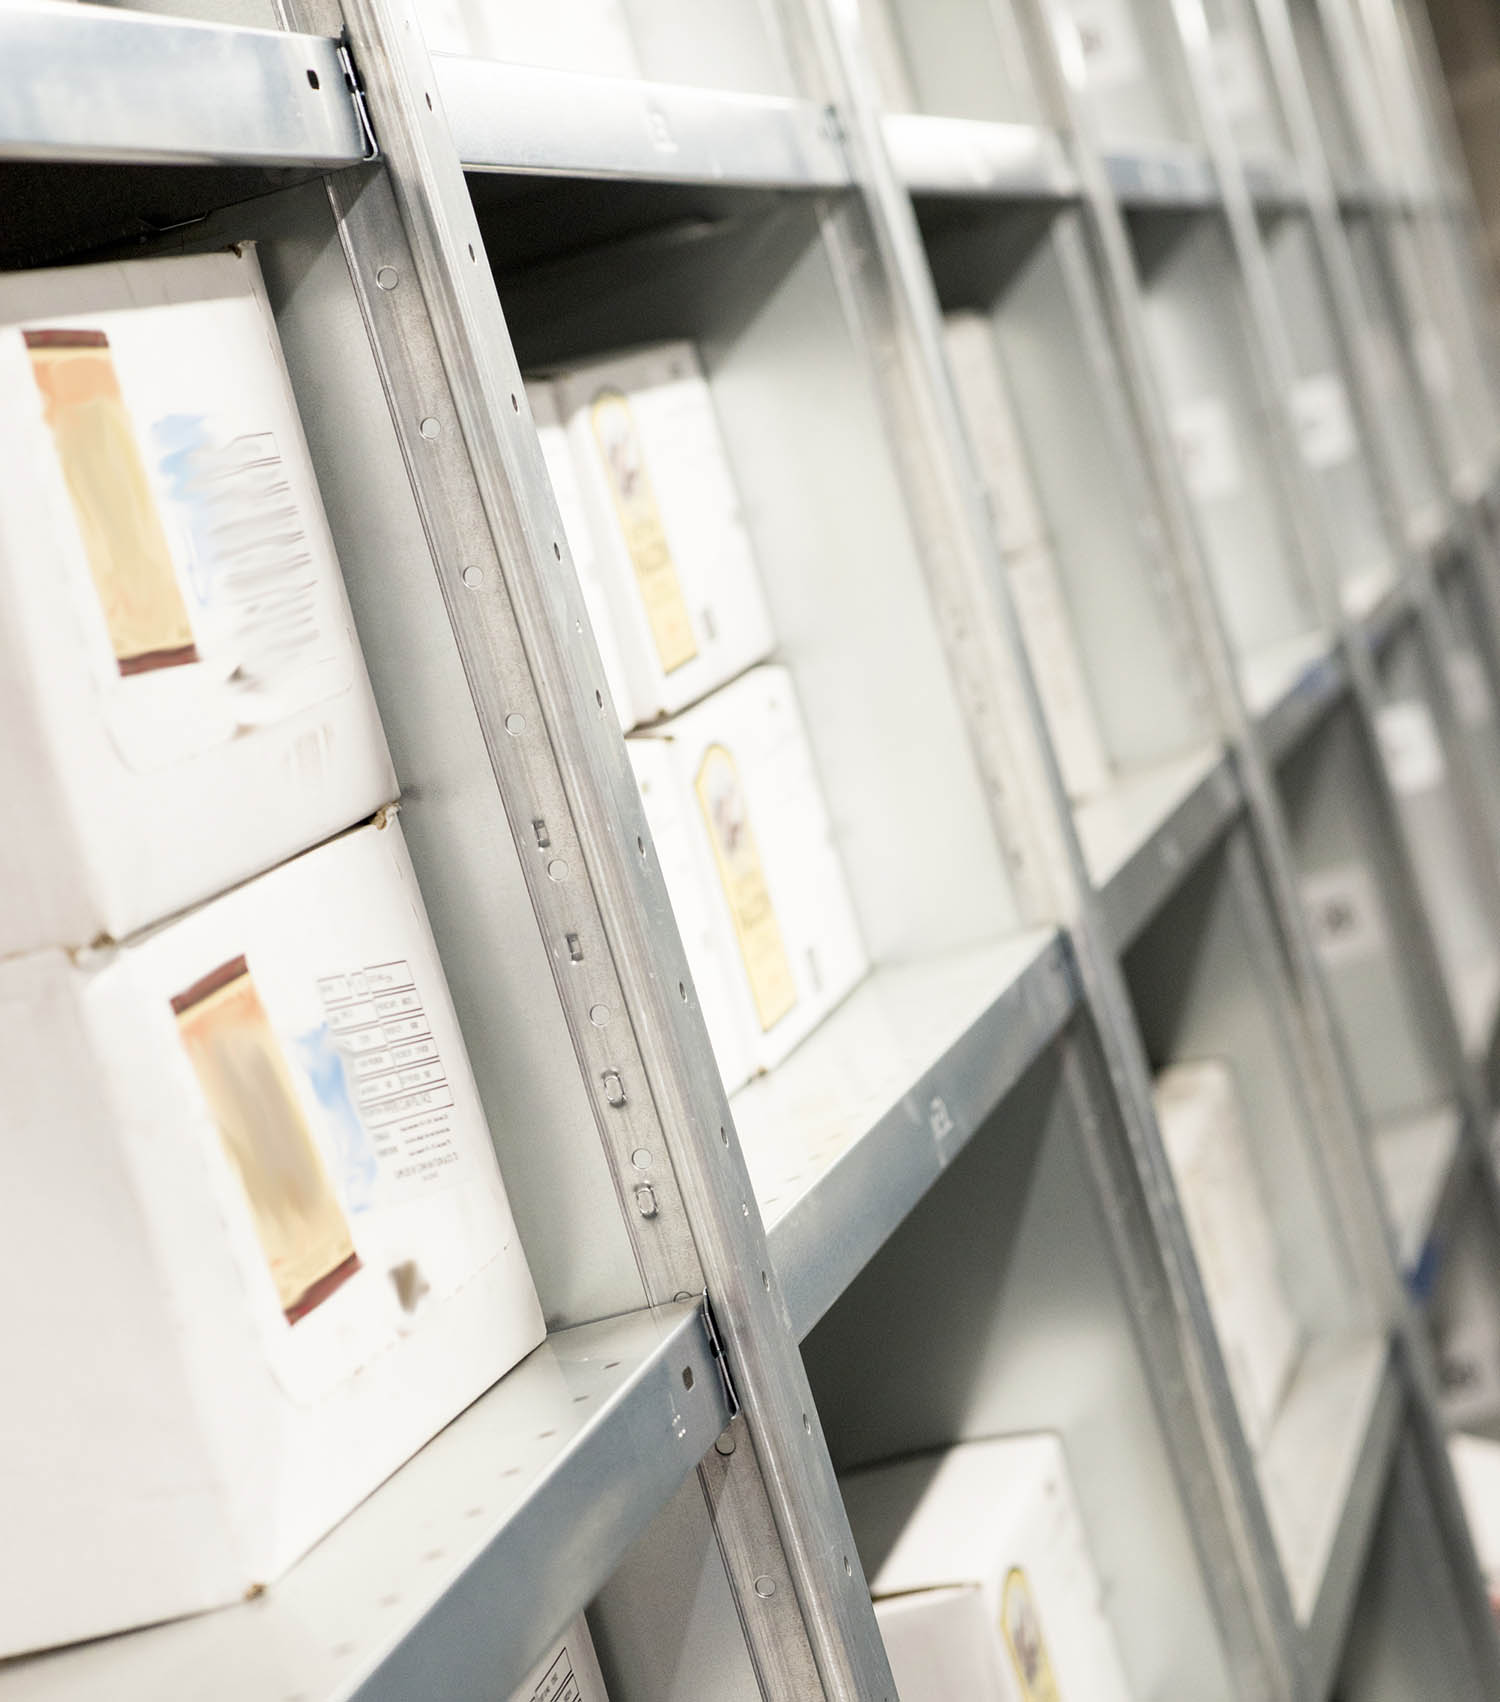
The client had been storing the labels and samples on wooden shelving and shelving in various areas across their facility and was looking to bring them together in one area to free up space in production areas.
Having seen examples of Thistle’s high density mobile label and samples stores, the client had anticipated this would be the perfect solution for their requirements.
However, after discussing the plans with Thistle’s whisky team and carrying out a site visit, Thistle proposed an alternative; the picking tower solution, which would not only provide an additional 200% capacity in the same floor space, but would also enable 100% accessibility to all labels and samples.
With an 8 metre ceiling height available and a relatively low speed of pick required, Thistle’s solution provided 96 bays of 1000mm wide shelving on the ground floor, 92 bays on the 1st and 2nd floor, each with 5 shelves per bay to deliver 1400 linear metres of storage in 100 square metres of floor space.
The client has the option to insert part or full height dividers to each location creating more pick faces.
Not only does this solution allow the client to increase their storage capacity but it also means that travelling times are greatly reduced between production and the products being stored as everything is contained in the one structure.
Security is also enhanced as there’s not as much of a flow of people – with only one entrance and exit, however the system has been designed to enable lockable security doors to be added at a later date.
Thistle’s experience in designing and building these solutions ensured that they met all building and fire regulations were met and the building warrant obtained.